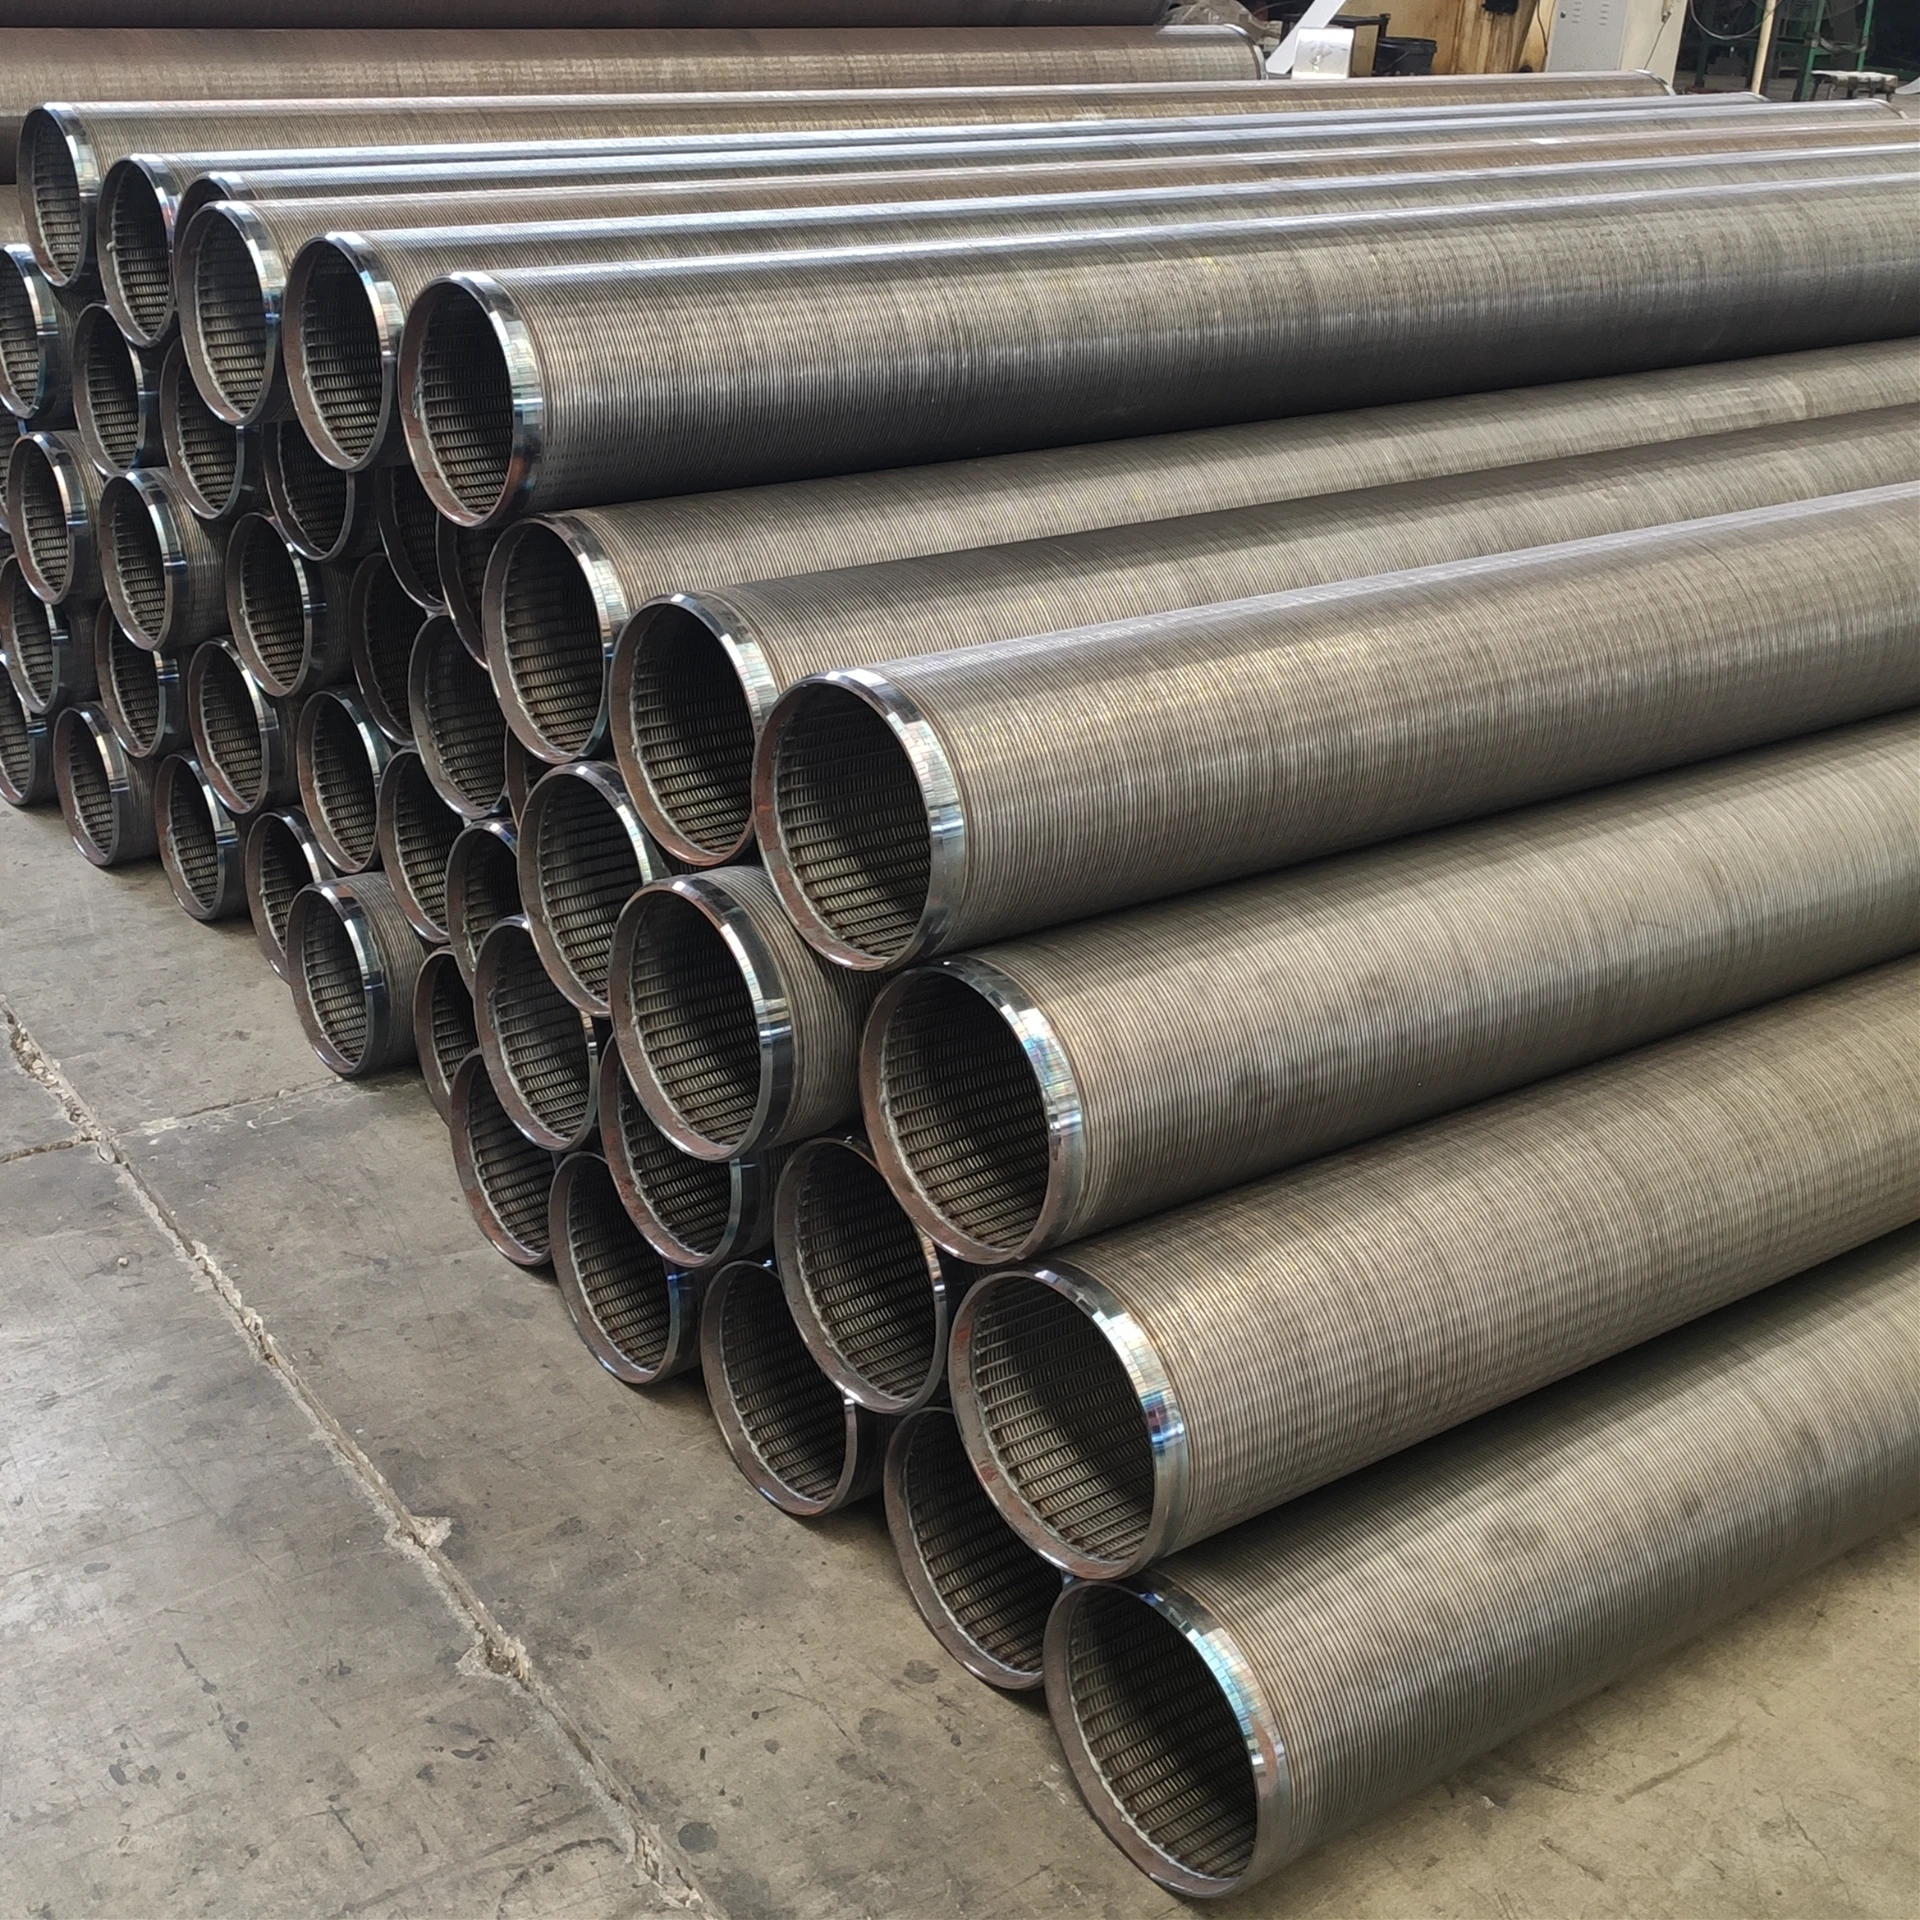
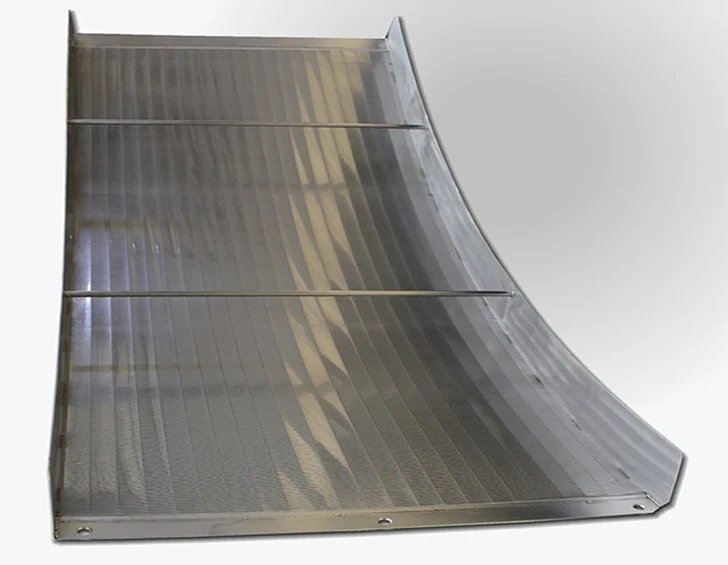
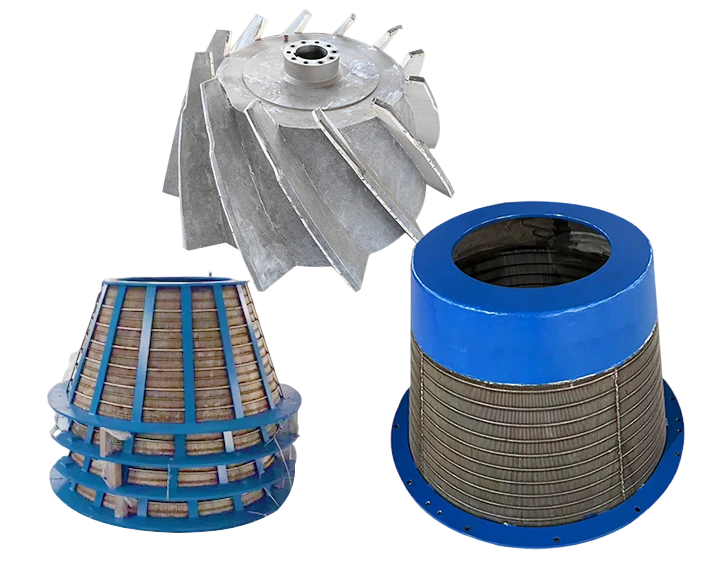
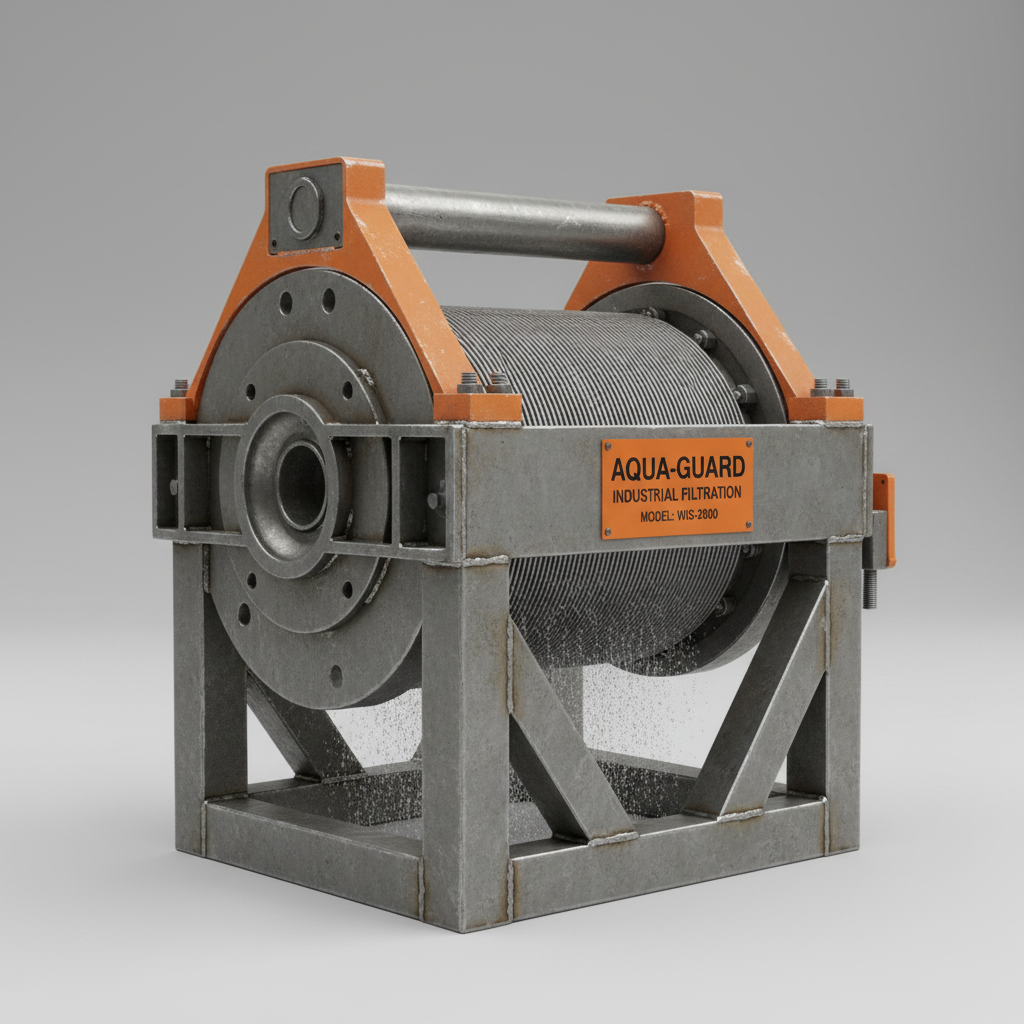
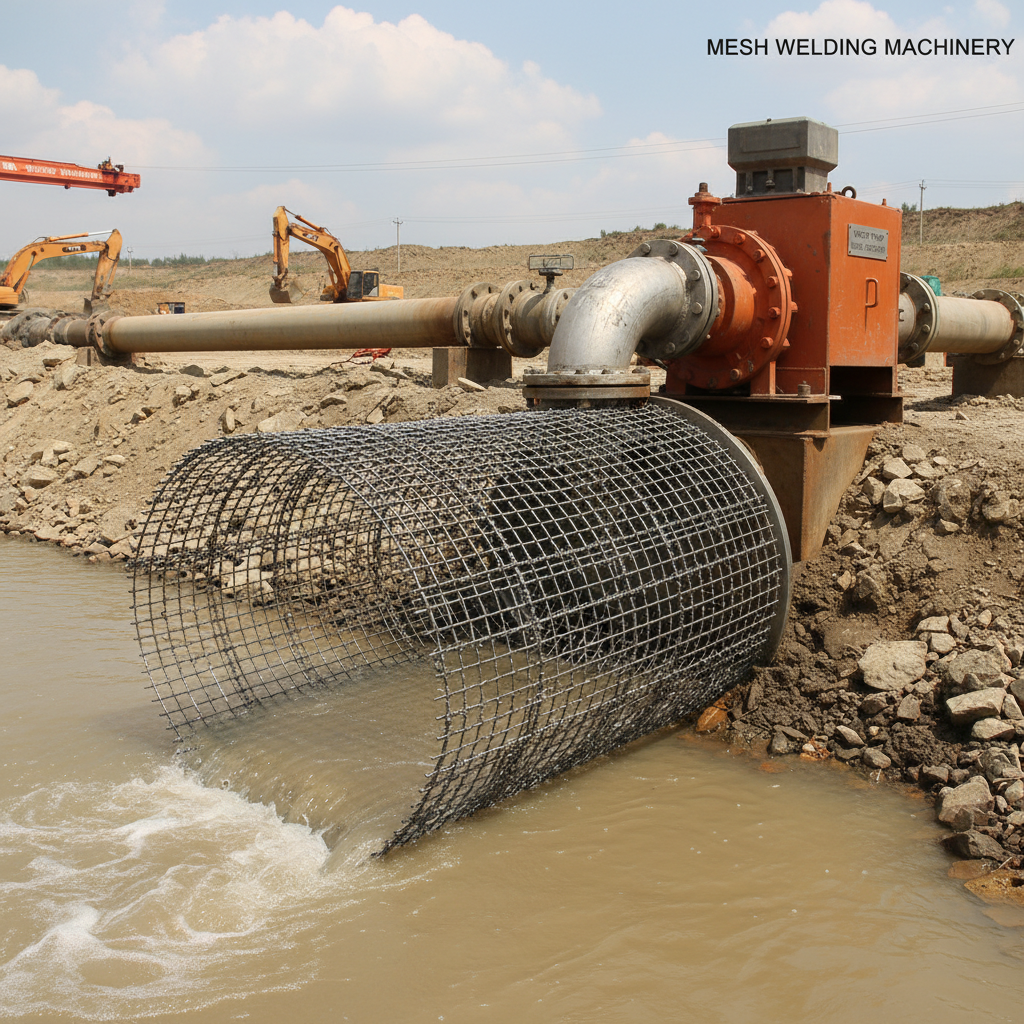
The efficiency of industrial filtration and fluid management often hinges on the precision of the screening equipment used. In the context of demanding environments, the implementation of a high-performance water well sand screen is essential for maintaining the purity of extracted resources and protecting downstream machinery from abrasive particulates. By effectively bridging the gap between raw extraction and refined processing, these systems ensure operational longevity and consistent output.
Across global mining and water management sectors, the challenge of clogging and material wear has historically led to significant downtime and increased maintenance costs. Modern engineering has responded with advanced polymer materials and strategic spray geometries that optimize the separation process. The transition toward durable, self-cleaning mechanisms represents a pivotal shift in how industries approach the complexities of sediment control and material washing.
Integrating a specialized water well sand screen into a production line allows for a more streamlined workflow, reducing the reliance on manual cleaning and frequent part replacements. This technological advancement not only enhances the throughput of minerals and chemicals but also ensures that environmental standards are met through more precise waste management and resource recovery.
Material Durability and Corrosion Resistance
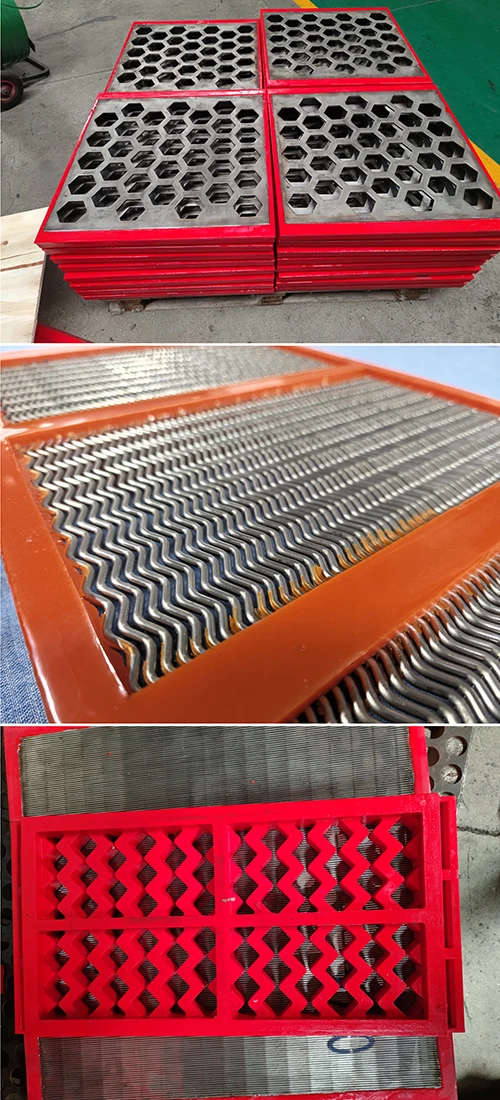
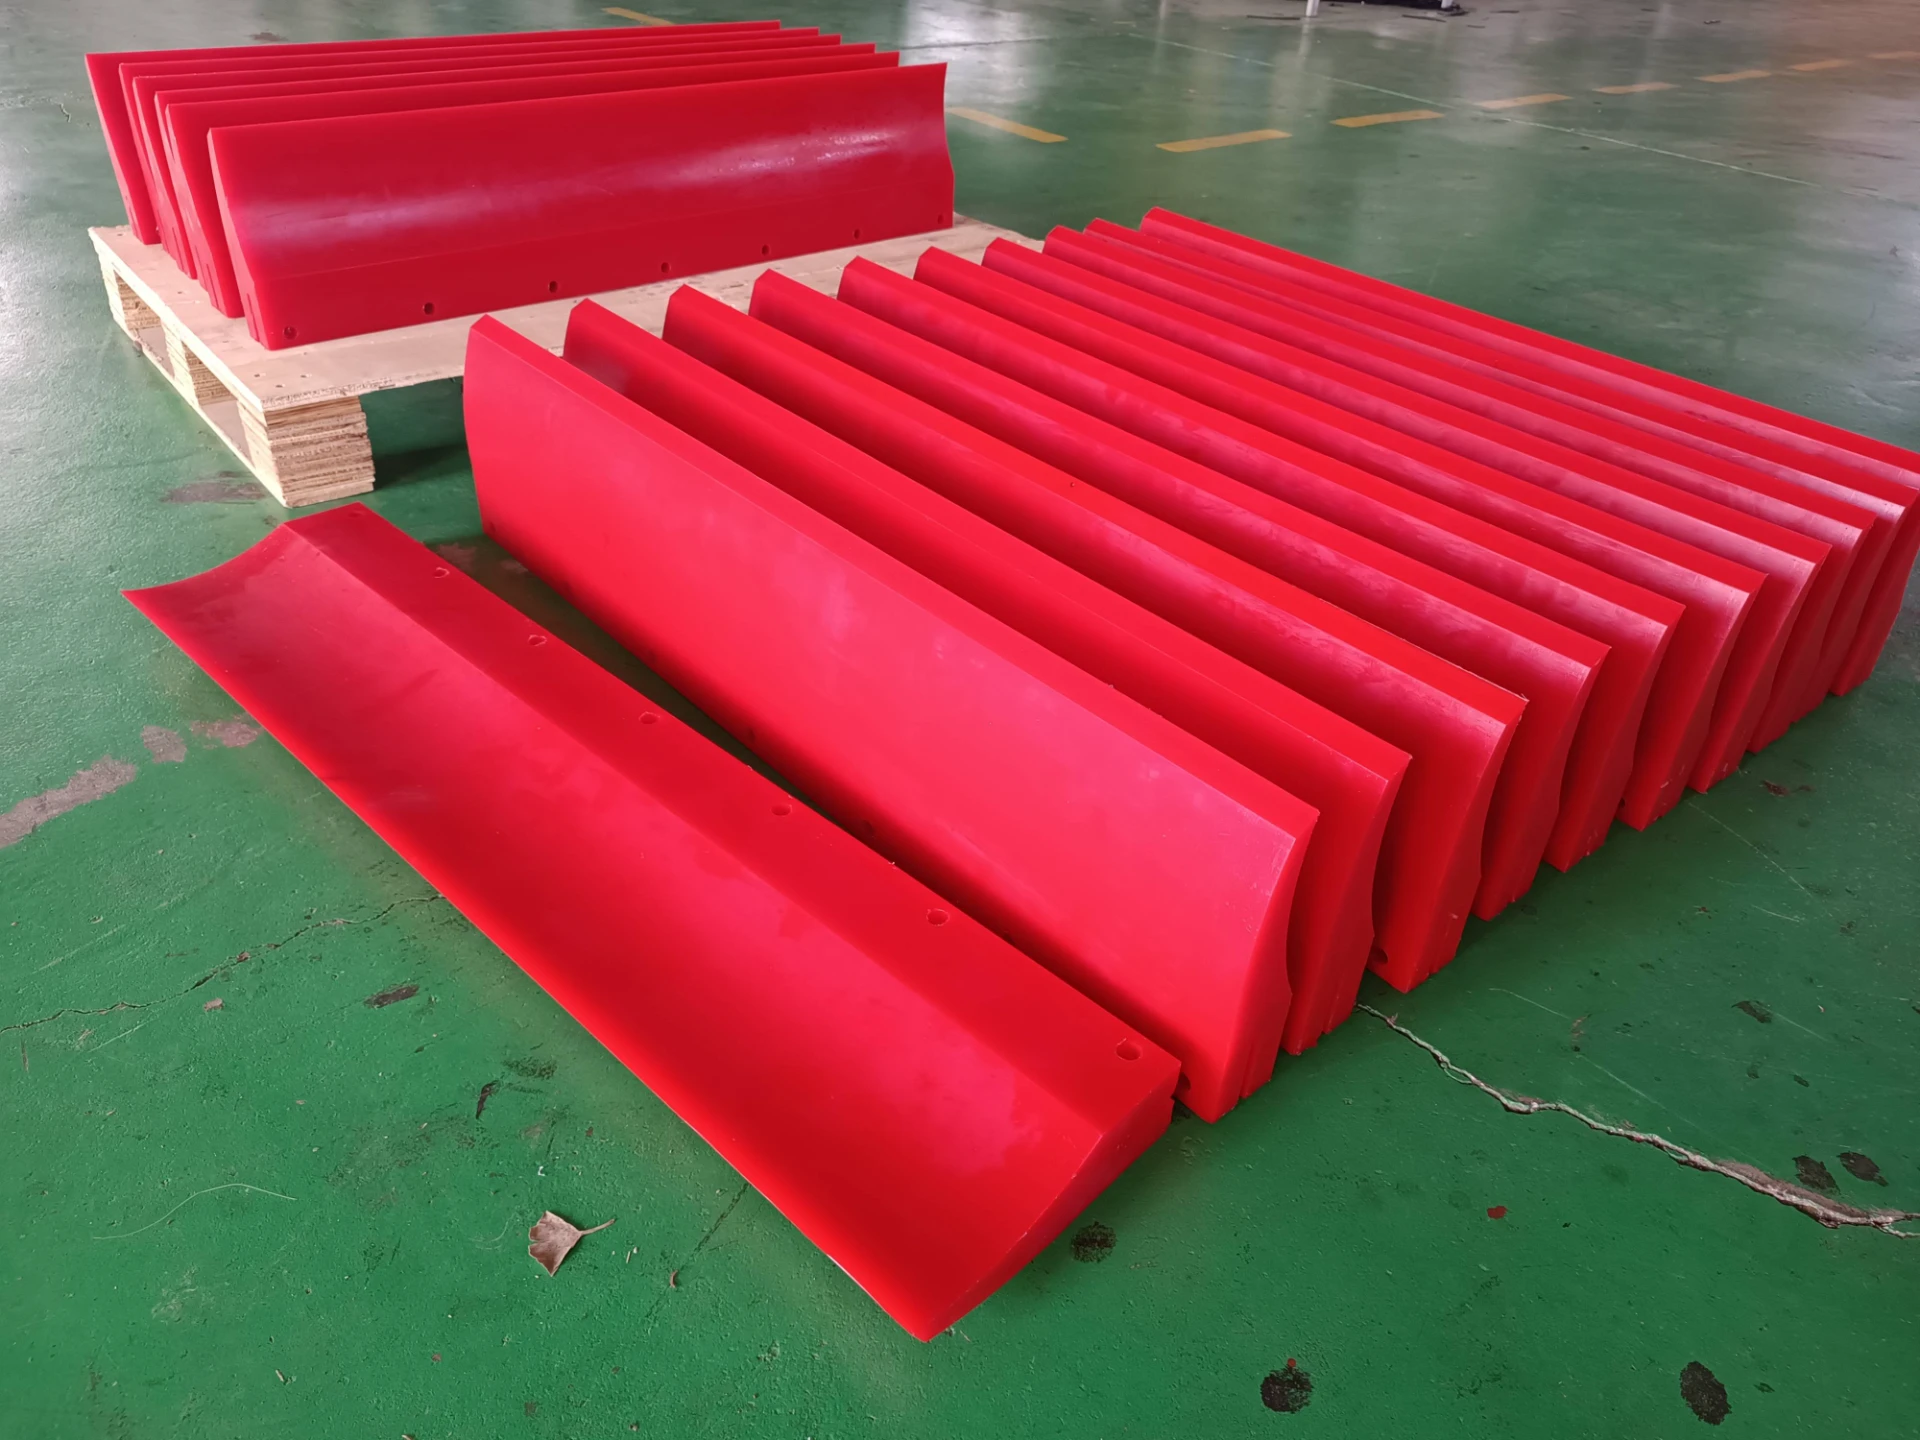
The foundation of any reliable water well sand screen lies in the quality of its construction materials. By utilizing high-density polyurethane and advanced durable polymers, these components are engineered to withstand the most aggressive environments. This is particularly critical in mining and chemical processing, where the constant friction of abrasive ores and the corrosive nature of industrial slurries can rapidly degrade standard metallic screens.
Polyurethane provides a unique combination of flexibility and hardness, allowing the screen to absorb impacts without cracking while maintaining a rigid structure to ensure precise separation. This inherent resistance to wear significantly extends the lifecycle of the equipment, reducing the total cost of ownership and minimizing the frequency of unplanned shutdowns.
The Mechanics of Self-Cleaning Design
Clogging is the primary enemy of efficiency in any filtration system. A well-engineered water well sand screen incorporates a self-cleaning design that prevents the accumulation of debris and fines on the screening surface. By utilizing fluid dynamics and specific aperture geometries, the system ensures that materials are continuously flushed through, maintaining a consistent flow rate without manual intervention.
This self-cleaning capability is achieved through the synergy of the material's low-friction surface and the strategic application of high-pressure water. When particles attempt to lodge within the screen, the constant movement and pressure differential force them through or wash them away, preventing the formation of "blinding" which typically plagues traditional mesh screens.
For operators in coal processing and waste management, this means a drastic reduction in maintenance labor. The ability to maintain a consistent separation efficiency over extended periods allows for a more predictable production schedule and ensures that the final output meets strict purity specifications.
Optimizing Flow with Fan-Shaped Spray Patterns
The integration of a fan-shaped spray pattern is a game-changer for the effectiveness of a water well sand screen. By creating a wide, consistent curtain of water, the system can distribute high volumes of liquid evenly across a 120-degree angle. This ensures that every inch of the screening surface is actively washed, eliminating dead zones where materials might accumulate.
When applying this technology to a water well sand screen, the 120-degree spray angle is optimized to maximize the separation of minerals and ores on screening decks. This precise distribution allows for the efficient removal of fine particles from larger aggregates, which is essential for high-grade mineral recovery in mining operations.
Furthermore, the high-volume water distribution reduces the overall residence time of materials on the deck, accelerating the throughput of the entire plant. This efficiency is not just about speed, but about the quality of the separation, as the fan-shaped spray ensures a thorough rinse that removes clinging contaminants from the target material.
Versatile Applications Across Global Industries
The utility of a water well sand screen extends far beyond a single application. In the mining sector, it is indispensable for washing and separating raw ores, while in coal processing, it facilitates the removal of fine coal particles to improve the caloric value of the final product. These systems are designed to handle the heavy loads and abrasive conditions typical of these heavy industries.
Beyond heavy industry, these screens are vital in food processing and the chemical industry. In food production, they ensure a hygienic and efficient separation of ingredients, while in chemical plants, they are used to filter slurries and chemicals with high reliability. Whether it is managing recyclables in waste management or purifying water in remote industrial zones, the adaptability of the design makes it a universal tool for material separation.
Performance Efficiency of Water Well Sand Screen Variants
Technical Specifications and Operating Pressures
Technical precision is the cornerstone of a high-functioning water well sand screen. These systems are typically designed to operate under high-pressure conditions, usually ranging from 50 to 200 PSI. This pressure is essential to drive the fan-shaped spray and maintain the self-cleaning action required to push heavy sediments through the polyurethane apertures.
To ensure seamless integration into existing infrastructure, various connection types are offered, including threaded, quick-connect, and flange options. This flexibility allows engineers to customize the installation based on the specific requirements of the site, ensuring a leak-proof and secure connection that can withstand the vibration and mechanical stress of industrial screening decks.
Long-Term Value and Operational Reliability
Investing in a premium water well sand screen provides tangible long-term value through the reduction of operational expenses. By minimizing the frequency of part replacements and reducing the man-hours spent on cleaning clogged screens, companies can significantly lower their O&M (Operations and Maintenance) budget. The reliability of high-density polyurethane ensures that the system performs consistently even under fluctuating load conditions.
From a strategic perspective, the increased uptime directly translates to higher profitability. In industries like mining and coal processing, where every hour of downtime can cost thousands of dollars in lost production, the dependability of a self-cleaning, wear-resistant screen is an insurance policy against unforeseen mechanical failures.
Moreover, the environmental impact is reduced as the increased efficiency of separation leads to better resource recovery and less waste. The trust built through consistent performance allows operators to scale their operations with confidence, knowing that their filtration infrastructure can handle increased volumes without compromising quality.
Future Trends in Polymer Screening Technology
The future of the water well sand screen is moving toward the integration of "smart" materials and digital monitoring. We are seeing a trend toward the development of polymers with embedded sensors that can detect wear patterns or clogging in real-time, allowing for predictive maintenance rather than reactive repairs. This shift toward Industry 4.0 will further minimize downtime and optimize the spray pressure based on the material density being processed.
Sustainability is also driving innovation, with a focus on creating biodegradable or fully recyclable high-performance polymers that do not sacrifice durability. As global environmental regulations tighten, the ability to implement a high-efficiency screening system that is also eco-friendly will become a competitive advantage for industrial operators.
Additionally, the refinement of 3D printing for polymer components allows for the creation of custom aperture geometries tailored to specific particle sizes. This level of customization will enable the water well sand screen to be perfectly matched to the specific ore or chemical slurry of a particular site, maximizing separation efficiency to near-theoretical limits.
Comparative Analysis of Polymer Screening Solutions
| Material Type |
Wear Resistance |
Cleaning Efficiency |
Expected Lifespan |
| Standard Polyurethane |
High |
Excellent |
2-3 Years |
| Reinforced Polymer |
Very High |
Excellent |
3-5 Years |
| Stainless Steel Mesh |
Medium |
Fair |
1-2 Years |
| TPE Composites |
Medium-High |
Good |
2 Years |
| Custom Hybrid Poly |
Extreme |
Superior |
5+ Years |
| Standard Plastic |
Low |
Poor |
0.5-1 Year |
FAQS
Polyurethane offers superior resistance to abrasion and corrosion compared to steel, especially in wet and chemically active environments. Its flexibility allows it to withstand impacts without permanent deformation, and its lower surface friction significantly reduces the likelihood of material clogging, leading to a longer operational lifespan and lower maintenance costs.
The fan-shaped spray creates a wide curtain of water across a 120-degree angle, ensuring that the entire surface of the water well sand screen is uniformly washed. This prevents the formation of material build-up in "dead zones," ensures that fine particles are efficiently rinsed away from larger materials, and increases the overall throughput of the screening deck.
To maintain the self-cleaning action and effective spray pattern, these systems are generally designed for high-pressure applications. The typical operating range is between 50 and 200 PSI. This ensures that the water has enough force to displace adhered particulates and maintain a consistent flow of materials through the screen.
Yes, they are highly versatile. In food processing, the durable polymers provide a hygienic surface for efficient separation. In the chemical industry, the corrosion-resistant nature of polyurethane allows the water well sand screen to filter aggressive chemicals and slurries without degrading, ensuring reliable performance in hazardous environments.
Depending on the abrasiveness of the material and the operating pressure, high-quality polyurethane screens typically last between 2 to 5 years. This is significantly longer than traditional metallic meshes, which may require replacement every 1 to 2 years due to corrosion or wear-through.
To accommodate various industrial setups, the water well sand screen is available with multiple connection types, including threaded connections for standard piping, quick-connect options for rapid maintenance, and flange connections for high-stability, heavy-duty industrial applications.
Conclusion
The implementation of an advanced water well sand screen, characterized by high-density polyurethane construction and a self-cleaning fan-shaped spray system, represents a critical upgrade for any industrial filtration process. By addressing the core challenges of material wear and clogging, these systems not only enhance the purity of the separated materials but also significantly reduce operational downtime and maintenance expenses. From mining and coal processing to chemical and food industries, the reliability and durability of these components ensure a sustainable and efficient workflow.
Looking forward, the evolution of screening technology will likely integrate smarter materials and more precise customization to further push the boundaries of separation efficiency. For organizations seeking to optimize their production lines and reduce long-term O&M costs, investing in high-performance polymer screening solutions is a strategic necessity. To learn more about our industry-leading solutions, visit our website: www.mutoscreens.com